Top 10 CNC Gundrilling Machine Suppliers Worldwide?
Choosing a Cnc Gundrilling Machine supplier is about more than comparing catalog prices. Deep-hole work depends on stable spindle performance, precise alignment, effective coolant delivery, and dependable chip evacuation. A small setup error can leave a long bore wandering off center. That matters when producing hydraulic components, aerospace parts, or precision shafts.
This guide compares ten suppliers worldwide through practical purchasing criteria: machine capacity, bore diameter range, automation options, controls, service coverage, and access to spare parts. Buyers should also ask for test-cut data using representative material and dimensions. A polished brochure is useful; a documented bore result is better. Check how each supplier handles installation, operator training, maintenance, and troubleshooting across your region.
Expert insight can sharpen a supplier comparison, but an attributed quotation should be verifiable. No source-backed statement from a named Cnc Gundrilling Machine specialist was provided for this draft, so it would be misleading to invent one. The comparison instead focuses on measurable questions buyers can take to vendors. Shortlist carefully. Confirm the details. Then match machine capability to the tolerances, production volume, and support your operation actually needs.
How CNC Gundrilling Machines Work and Where They Are Used
A CNC gundrilling machine produces long, narrow holes with controlled position and diameter. The cutting tool has an internal coolant passage, which delivers fluid near the cutting edge. Coolant helps manage heat and carries chips back through the flute. The CNC system controls tool feed, rotation, and travel, while the setup keeps the workpiece and drill aligned. That matters. A small alignment error can cause a bore to wander, especially as drilling depth increases. Operators still need to select suitable speeds, feeds, and coolant conditions for the material. Automation helps, but it does not remove the need for careful setup.
These machines are used for parts such as hydraulic components, fuel-system pieces, shafts, and precision tooling. Aerospace and automotive manufacturers may use them when a deep, straight passage is needed inside a metal component. A shop might drill a narrow channel through a steel shaft, then inspect the bore for position, finish, and size. Results depend on the workpiece, tool condition, and machine setup; one parameter set will not suit every job. This is easy to underestimate. Chips, heat, and tool wear can change the outcome, so routine checks matter. CNC control offers repeatability, but the process still rewards experienced judgement.
Top 10 CNC Gundrilling Machine Suppliers Worldwide? - How CNC Gundrilling Machines Work and Where They Are Used
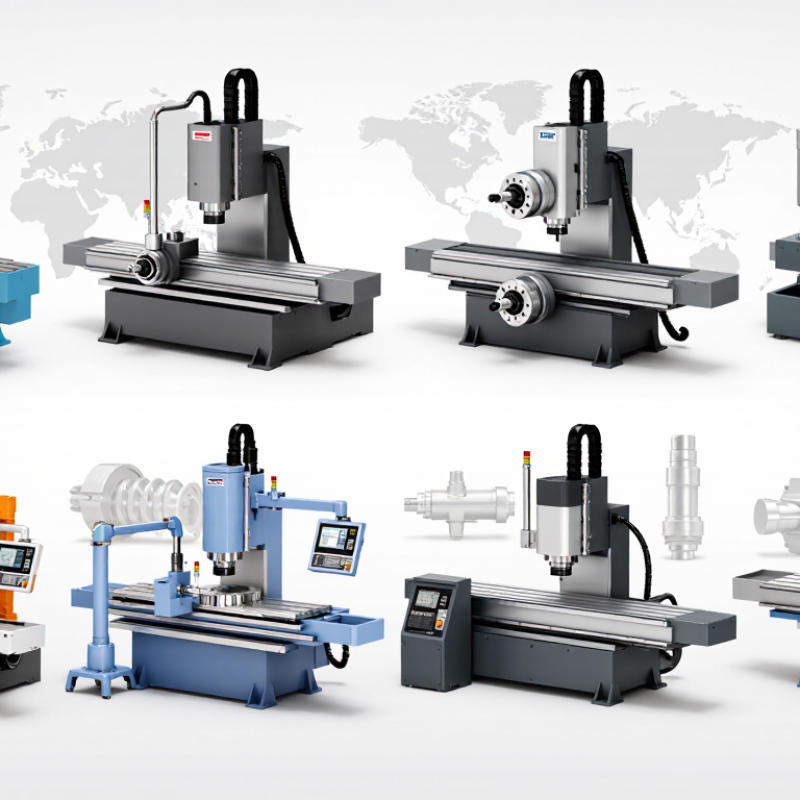
This is an anonymized overview of ten supplier categories and their typical capabilities—not a ranked directory of named companies. Machine capacity varies by model, tooling, material, and process setup; confirm specifications with the supplier.
| # | Supplier category | Typical machine or service | How the process works | Common applications | What to verify when sourcing |
|---|---|---|---|---|---|
| 1 | Dedicated gundrilling machine builders | Purpose-built CNC machines for long, straight, relatively small-diameter holes. | A rotating workpiece, rotating tool, or both may be used. High-pressure coolant passes through the tool to carry chips out of the hole. | Molds, dies, hydraulic components, and precision shafts. | Working diameter and depth range, axis configuration, coolant pressure and filtration, and demonstrated hole straightness. |
| 2 | Deep-hole drilling system integrators | Configured drilling cells combining a machine, workholding, coolant equipment, and controls. | The integrator matches the drilling method and machine layout to the part, then coordinates coolant delivery and chip evacuation. | Long components, production cells, and parts with specialized loading or fixturing needs. | Scope of integration, acceptance testing, process responsibility, and support for the complete cell. |
| 3 | Multi-spindle and high-production machine suppliers | Machines designed to drill several holes or parts in parallel, where the job permits. | CNC motion and synchronized spindles feed gundrills into the work while coolant supports cutting and chip removal. | Repeat production of components with multiple deep holes and stable part geometry. | Spindle count, simultaneous capacity, setup time, repeatability, and changeover requirements. |
| 4 | Small-diameter precision drilling specialists | Fine-hole gundrilling equipment and process support for small bores. | A guided, single-flute gundrill and controlled coolant flow help maintain cutting stability and remove chips from a narrow bore. | Fuel-system parts, medical components, precision instruments, and small hydraulic passages. | Minimum practical diameter, tool availability, runout control, bore finish, and inspection method. |
| 5 | Large-workpiece and heavy-duty machine suppliers | Long-bed or heavy-capacity machines for large, long, or heavy workpieces. | The workpiece is supported and aligned; the CNC-controlled tool feed and coolant system sustain drilling over a long travel. | Power-generation components, large shafts, industrial cylinders, and oversized tooling. | Maximum workpiece mass and length, support arrangement, travel, foundation needs, and loading method. |
| 6 | Combination deep-hole drilling machine suppliers | Machines that can be configured for gundrilling and other deep-hole methods, such as BTA drilling. | The selected method depends on bore size, depth, material, and production requirements; each method has different tooling and chip-removal arrangements. | Job shops and manufacturers handling varied deep-hole part families. | Supported processes, changeover effort, method-specific capacity, and tooling and coolant requirements. |
| 7 | Custom-machine and special-purpose builders | Machines engineered around unusual part geometry, access constraints, or production sequences. | Custom fixturing and CNC motion position the part and tool so the bore can be drilled with controlled feed and coolant flow. | Complex castings, angled passages, dedicated production lines, and nonstandard components. | Design validation, process trials, documentation, service access, and future modification costs. |
| 8 | Retrofitting and CNC modernization providers | Upgrades to controls, drives, safety systems, coolant equipment, or automation on existing machines. | Modernized controls coordinate feed and spindle functions; upgraded coolant and filtration equipment can support the drilling process. | Plants seeking to extend the useful life or improve the operation of existing deep-hole equipment. | Mechanical condition assessment, compatibility, safety compliance, warranty, and post-upgrade testing. |
| 9 | Machine-tool distributors with application engineering | Local sales, installation, training, and application support for deep-hole drilling equipment. | Application engineers review the part and process requirements, then help specify a suitable machine, tooling, and coolant package. | Manufacturers needing local commissioning, training, or ongoing technical assistance. | Local service coverage, spare-parts availability, engineer experience, and clarity on who provides technical support. |
| 10 | Contract deep-hole drilling service providers | Outsourced drilling services for customers who do not need to own a dedicated machine. | The service provider selects tooling and cutting conditions, drills the specified bores, and inspects them to the agreed requirements. | Prototype work, low-volume production, and overflow capacity for long-hole parts. | Material handling limits, dimensional inspection capability, lead time, traceability, and quality documentation. |
Where gundrilling is used: The process is commonly selected for straight, deep holes in components used in aerospace, automotive, energy, medical, hydraulic, mold-and-die, and general industrial manufacturing. Actual suitability depends on part material, bore geometry, tolerances, and production volume.